
Control panel power supply selection
A 24 VDC supply is more than voltage and amperage
A calculated 7 amp panel load can make a 10 amp, 24 VDC supply look like an easy selection. Under steady operation, that may be true. The real question is how the supply behaves when devices start together, a capacitive load energizes, incoming power sags, or one branch circuit faults.
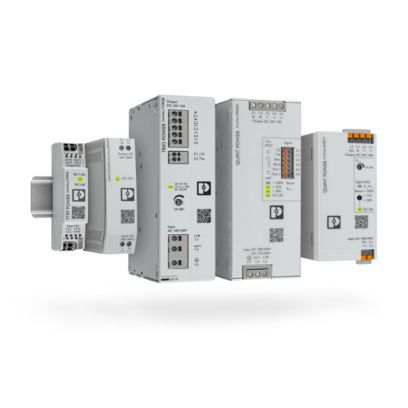
Phoenix Contact offers UNO POWER, TRIO POWER, and QUINT POWER families for different application needs. Selecting between them should be an engineering decision based on load behavior, system availability, diagnostics, fault clearing, and future serviceability.
The problem with nameplate-only selection
Voltage and continuous current are necessary checks, but they do not describe startup reserve, overload behavior, short-circuit response, monitoring, or how one failed field circuit affects the rest of the panel. A supply that is acceptable for a small steady load may be a poor fit for a pump station, process panel, or remote system where losing the 24 VDC bus creates downtime and confusing fault symptoms.
UNO POWER
Compact basic power for stable, predictable loads. UNO can fit small enclosures and dedicated auxiliary equipment where advanced monitoring or selective fault clearing is not required.
- Small instrumentation panels
- Remote monitoring enclosures
- Operator interfaces or communication devices
- Constant, noncritical DC loads
TRIO POWER
Standard industrial power for machine and system loads with more dynamic behavior. TRIO can be appropriate where reserve capability, diagnostics, and cost balance matter.
- Machine control panels
- Conveyor and solenoid systems
- Distributed I/O panels
- Moderate startup demand
QUINT POWER
Maximum-functionality power for critical applications where reserve, diagnostics, configurable behavior, and fault-clearing support can protect system availability.
- Municipal water and wastewater systems
- Lift and pump stations
- Remote unattended panels
- Processes where restarting is difficult
Why fault current matters
Consider a panel with separate DC branches for the PLC, remote I/O, operator interface, network switch, instrumentation, relays, solenoids, and field devices. If one field cable shorts, the preferred result is for the protective device on that branch to trip quickly while the unaffected control circuits remain powered.
A current-limiting supply may reduce output before a standard miniature circuit breaker receives enough current to trip magnetically. The faulted branch then drags down the whole 24 VDC bus while protection responds slowly or the control system resets first.
Selective Fuse Breaking is a system design tool
Phoenix Contact describes QUINT POWER supplies with SFB Technology as supporting selective tripping of standard miniature circuit breakers so parallel loads can continue operating. The actual result still depends on the exact supply, breaker curve and rating, conductor size, wire length, connection resistance, and available short-circuit current.
When QUINT is worth specifying
One fault should not stop everything
In a coordinated design, a QUINT supply can help provide the short-duration current needed to clear a faulted branch while preserving power to PLCs, communications, and unaffected loads.
Temporary load demand matters
Some industrial computers, HMIs, network equipment, capacitive devices, solenoid banks, radios, and I/O assemblies demand more current during startup than during normal operation. Power reserve can support these events without simply oversizing continuous capacity.
Monitoring provides earlier warnings
More advanced supplies can provide status and signaling that help identify output voltage, current, reserve, or overload concerns before the DC bus fails and the root cause becomes harder to separate from the shutdown.
Future changes are likely
Panels often gain instruments, radios, Ethernet switches, I/O modules, relays, and monitoring equipment over time. A supply with useful reserve and diagnostics gives the system a better foundation for those additions.
When TRIO or UNO may be the better choice
TRIO may fit
TRIO POWER can be the right balance when the application has dynamic loads but limited consequences from a complete shutdown, moderate boost capability is enough, extensive preventive monitoring is unnecessary, and panel cost is a major constraint.
UNO may fit
UNO POWER can be the correct selection when the load is small and predictable, little starting current is required, DIN rail space is tight, the supply serves a dedicated device, and branch-circuit selectivity is not required.
Good engineering does not mean using the most expensive supply in every enclosure. It means matching the operating behavior of the power supply to the risk, load profile, and service expectations of the control system.
Questions to ask before selecting
- What is the normal continuous load?
- What is the maximum expected load?
- Are connected devices highly capacitive?
- Do loads have significant startup or inrush current?
- How much future expansion is expected?
- What happens if the 24 VDC bus shuts down?
- Must one failed branch be isolated while other circuits continue operating?
- What type and size of branch protection will be used?
- Are wire lengths and conductor sizes compatible with selective tripping?
- Does the PLC need advance warning of an overloaded power system?
- Is redundancy required?
- How difficult or expensive would restart be?
How can BEA help?
Britton Electronics & Automation can help evaluate control-panel power calculations, Phoenix Contact UNO, TRIO, and QUINT selection, DC branch-circuit coordination, breaker or electronic protection selection, voltage drop, redundancy, PLC monitoring, modernization, and recurring 24 VDC failures.
The right supply is not selected only for the day everything works normally. It is selected for how the panel should behave when a field circuit fails, a load starts hard, or the system grows beyond its original assumptions.
For additional manufacturer context, see Phoenix Contact's overview of power supplies, SFB Technology, and QUINT POWER maximum-functionality supplies.
Power factor is a capacity and efficiency signal
In an AC power system, some current does useful work and some current supports magnetic fields in equipment such as induction motors, transformers, and contactor coils. Power factor describes how much of the supplied apparent power is converted into real work at a given operating point.
A low power factor does not mean the motor is doing more mechanical work. It usually means the electrical system is carrying more current than necessary for the useful output being delivered.

What is power factor?
Power factor is the ratio between real power, measured in kilowatts (kW), and apparent power, measured in kilovolt-amperes (kVA). Reactive power, measured in kVAR, is the portion that circulates between the source and reactive loads without producing mechanical output.

The power triangle
The triangle is a useful way to explain the relationship: kW is useful work, kVAR is reactive demand, and kVA is the total electrical capacity the distribution system must support.

Lagging current
Many inductive loads draw current that lags voltage. The larger that phase difference becomes, the lower the displacement power factor becomes.
Why does power factor matter?
Good power factor
- Lower current for the same useful work
- Less heating in feeders, transformers, and switchgear
- Lower voltage drop under load
- More usable electrical capacity for production equipment
Poor power factor
- Higher current for the same useful work
- More I-squared-R losses and equipment heating
- Greater voltage drop during heavy loading
- Less available capacity before conductors or transformers reach limits
Utilities may also measure demand in ways that penalize poor power factor. Even when there is no direct penalty, low power factor can still consume distribution capacity that could otherwise support additional loads.
Capacitor banks
Capacitor banks are a common correction method for inductive loads. When applied correctly, they supply part of the reactive power locally, so less reactive current has to travel from the utility source through upstream conductors and transformers.
Before correction
The utility and upstream distribution equipment supply both real current and reactive current to the load. Feeders and transformers carry the combined current, which can increase heating and voltage drop.

After correction
A properly engineered capacitor bank near the load supplies reactive power locally. The motor mechanical load is unchanged, but upstream current can be reduced.
Do not confuse displacement power factor with harmonics
A facility with variable frequency drives may show good displacement power factor while still having harmonic distortion on the input current. That is why a power-quality review should look beyond a single power factor number when drives, rectifiers, or other nonlinear loads are present.
When to investigate power factor
- Utility bills show power factor penalties, kVA demand charges, or unexplained demand increases.
- Transformers, feeders, or switchgear are warm under normal production loading.
- Voltage drop appears when large motors, pumps, or blowers start or operate together.
- A facility is adding equipment and needs to understand available electrical capacity.
- Existing capacitor banks, contactors, or controllers are aging, disabled, or frequently faulting.
How BEA can help
BEA can help evaluate the practical side of power factor in industrial automation environments: reviewing electrical drawings, checking motor and drive applications, coordinating with qualified electrical personnel, and supporting power-quality measurements where appropriate. The right answer may be correction equipment, a settings or maintenance issue, a drive or harmonic review, or simply better visibility into how the electrical system behaves under real production load.
For facilities with motor-control centers, VFDs, pumps, blowers, and mixed automation loads, the best starting point is a measured assessment. That keeps recommendations tied to actual current, voltage, demand, and operating conditions instead of assumptions.
Selected illustration sources are public Wikimedia Commons files used as attributable technical image candidates; final image approval and licensing review should occur before publishing.
Motor control selection
VFD vs. Soft Starter: Why a VFD Can Be the Better Choice, Even at Full Speed
When planning a new pump installation or upgrading an existing motor control system, a common question is whether a variable frequency drive is worthwhile when the motor is expected to run at full speed. The answer depends on more than the start sequence.
The common question
Soft starters and variable frequency drives are often compared because both can reduce the electrical and mechanical shock associated with starting a motor. For a simple application that only needs controlled acceleration and then runs directly across the line, a soft starter may be a suitable and economical option.
A VFD, however, does not stop adding value once the motor reaches 60 Hz. Even in constant-speed operation, the drive continues to manage the motor, monitor operating conditions, and provide information that can support troubleshooting and long-term system planning.


Mechanical stress still matters
Smooth acceleration and deceleration can reduce stress on pumps, bearings, couplings, belts, gearboxes, and piping systems. Even when the normal operating point is full speed, a controlled ramp can help reduce shock loads during starting and stopping.
Control system integration
Modern facilities increasingly depend on PLCs, HMIs, SCADA systems, and remote monitoring. A VFD can provide more than a run status bit. Depending on the drive and network options, operators may be able to monitor speed, current, power consumption, drive temperature, fault history, and operating status.
That information helps maintenance and operations teams see how the equipment is performing, not just whether it is running.
Practical selection checks
Which one is right?
There is no universal answer. If the application is simple, has minimal monitoring requirements, and is unlikely to require speed control, a soft starter may be the most economical choice.
When long-term flexibility, diagnostics, equipment protection, and integration with modern automation systems are priorities, a VFD often delivers greater operational value, even if the motor spends most of its life at full speed.
How can BEA help?
BEA can help evaluate the application, motor, pump curve, control requirements, available power, enclosure needs, communication options, and maintenance expectations before a starter or drive is selected. The best choice should account for today's operating requirement and the changes the system may need to support later.
For additional manufacturer context, see Rockwell Automation's overview of PowerFlex low-voltage AC drives and SMC-50 soft starters.
BEA Blog
Why proper grounding is the foundation of a reliable control system
When an operator sees intermittent communication faults, unexplained PLC issues, inaccurate instrumentation, or nuisance VFD trips, it is natural to start with the device that appears to be misbehaving. In many facilities, the better first question is more basic: does the grounding system still provide a stable reference for the controls equipment?

Grounding does more than provide safety
Most people think of grounding strictly as a safety requirement, and that remains essential. For automation systems, grounding also gives sensitive electronics a stable electrical reference. PLCs, HMIs, VFDs, flow meters, level instruments, and industrial networks all rely on clean signals. When the grounding system is weak, noisy, corroded, or poorly bonded, those signals can become difficult to trust.
Common symptoms of grounding problems
Poor grounding can look like several different failures at once: intermittent PLC faults, random communication losses, erratic level readings, unstable flow measurements, drifting analog signals, nuisance VFD trips, Ethernet errors, or equipment resets after nearby lightning events. The frustrating part is that these symptoms are often sporadic, so replacing one component at a time may not solve the real problem.
Modern equipment is more sensitive
High-speed processors, Ethernet/IP networks, precision instruments, remote monitoring hardware, wireless devices, and VFDs all increase the importance of noise control and reference stability.
Ground resistance matters
Soil conditions, corrosion, damaged conductors, and aging ground rods can raise resistance over time. Routine testing helps catch changes before they become operational problems.
Good grounding is a system
Bonding, conductor sizing, low-resistance connections, surge protection, shield termination, and manufacturer-recommended installation practices all work together.
Do not chase symptoms without checking the foundation
When automation faults repeat, replacing sensors, PLC modules, drives, or network hardware may only hide the issue temporarily. If the underlying grounding problem remains, the same behavior can return later. Reviewing grounding health can reduce unnecessary part replacement, shorten troubleshooting time, and improve long-term system reliability.
A strong foundation for reliable automation
Reliable automation starts before the PLC program is written and before the first motor is started. A properly designed and maintained grounding system supports stable signals, safer installations, and longer equipment life. Whether a team is commissioning a new facility or maintaining an existing one, grounding deserves the same practical attention as controls programming, panel design, network layout, and instrumentation selection.
How can BEA help?
BEA can help review grounding-related symptoms in the context of the full control system, including PLCs, VFDs, instrumentation, networks, surge protection, bonding, panel practices, and field wiring. When the problem is intermittent, a structured review helps separate a failed device from a system condition that is affecting multiple devices.
Industrial Communications | Long-Term System Design
Why Open Protocols Matter in Industrial Automation
The way devices communicate can shape the cost, flexibility, and useful life of an automation system just as much as the hardware itself.

The overlooked design decision
Hardware choices matter. Communication architecture lasts longer.
When designing an industrial automation system, most people focus on PLCs, HMIs, variable frequency drives, instrumentation, and network equipment. Quality hardware is important, but the protocols connecting those devices often determine how easily the system can be maintained, expanded, and modernized.
What is an open protocol?
An open protocol is a publicly documented communication standard supported by multiple manufacturers. Rather than requiring one vendor's proprietary hardware or software, it lets equipment from different suppliers exchange information using a common language.
Widely used examples include Modbus RTU, Modbus TCP, EtherNet/IP, OPC UA, MQTT, and DNP3. Each serves different applications, but broad industry support gives facility owners more choices when designing, expanding, or servicing a system.
Choice
Reduce vendor lock-in
Proprietary communications can require specialized hardware, licensed software, or service from a single source. An open architecture gives owners access to multiple qualified suppliers and service providers, allowing decisions to be based on performance, availability, and cost.
Growth
Plan for future expansion
Industrial facilities rarely remain unchanged. Open standards can make it easier to add instrumentation, increase production, expand treatment processes, and upgrade equipment without redesigning the entire communications architecture.
Fit
Select better equipment
Engineers should be able to select a device because it meets the operational requirements, not because it is the only product capable of talking to an existing system. Open protocols broaden the field of proven industrial options.
Easier troubleshooting, less downtime
Standard protocols are familiar to technicians, engineers, and system integrators across the industry. Documentation, diagnostic software, and training resources are more widely available, making communication problems easier to identify and replacement equipment easier to source.
Service teams are less dependent on proprietary diagnostic tools, which can shorten troubleshooting time and help restore operations faster.
Protecting a long-lived investment
Automation systems often remain in service for twenty years or more. During that time, computers, operating systems, servers, networking equipment, and software platforms will continue to evolve.
A system built around open communication standards is better positioned to adapt without complete replacement. Individual components can often be modernized while preserving the overall architecture, extending useful life and reducing future modernization costs.
Building systems that last
Long-term value should not create long-term limitations
Open communication protocols help facilities remain flexible, maintainable, and prepared for future expansion. They reduce dependence on proprietary solutions while giving owners greater control over how their systems are serviced and upgraded.
A well-designed automation system should continue serving the facility for decades. Choosing open standards during design is one of the best ways to help make that possible.
Rittal | Industrial Enclosures
VX Hybrid Double Door: Strength That Can Move with the Job
A new U.S.-built enclosure system combines rugged construction, modular flexibility, and practical two-person portability.

New from Rittal
A hybrid approach to demanding installations
Announced in April 2026, the VX Hybrid Double Door applies Rittal's modular enclosure philosophy to a standalone, closed system. It is designed for operations that need dependable equipment protection without turning every move or field deployment into a heavy handling project.
Made in Ohio for tough industrial environments
Rittal produces the enclosure in Urbana, Ohio. The company positions it for mining and construction, utilities, oil and gas, water and wastewater, food and beverage, outside plant, energy and energy storage, agriculture, and pulp and paper applications.
Carbon-steel versions provide a NEMA 4 option, while stainless-steel versions provide a NEMA 4X option for applications that need added corrosion resistance.
Portability
Two-person handling
The streamlined frame is designed so two people can reposition the enclosure without the extra handling demands associated with traditional heavy systems.
Installation
Faster panel access
A single-footprint frame minimizes on-site assembly, and the removable center mullion simplifies adding the mounting panel.
Flexibility
VX25 compatible
Compatibility with the VX25 accessory platform supports customization and future changes as field requirements evolve.
Rigid protection without unnecessary handling weight
Rittal uses a rigid, fold-over frame engineered to provide strength comparable to traditional heavy-gauge steel construction while remaining manageable for field teams. The combination is intended to protect critical components in harsh locations while improving mobility, installation, and service access.
Read the official announcement: Rittal launches the VX Hybrid Double Door enclosure system.
Plan the complete enclosure
BEA can help match the enclosure to the application
Britton Electronics & Automation can help evaluate enclosure material, environmental rating, dimensions, internal layout, mounting, climate control, power distribution, and accessories as part of the wider controls package.
Contact BEA to discuss a new panel build, field installation, or enclosure upgrade.
Tolomatic | Extreme Force Electric Motion
RSX50: 50 Tons of Precise Electric Force
The newest RSX actuator doubles the force capacity of the RSX25 while keeping a remarkably similar footprint.

New from Tolomatic
Hydraulic-class power, electric control
Built around Tolomatic's high-precision planetary roller-screw technology, the RSX50 is designed for high-force, high-cycle work where manufacturers want measurable motion and force without hydraulic leaks, fluid handling, and maintenance complexity.
A major jump in power density
Tolomatic rates the RSX50 for maximum force of 100,000 lbf (445 kN), twice the 50,000-lbf rating of the RSX25. Maximum published stroke is 25 inches (630 mm), and maximum speed is 17 in/sec (432 mm/sec).
Its compact high-force package opens an electric path for pressing, punching, stamping, timber processing, injection molding, and other demanding industrial processes traditionally served by hydraulics.
Force
100,000 lbf
Up to 50 tons of controlled linear force for heavy industrial duty.
Stroke
Up to 25 in
A published maximum of 630 mm, with extended options available by request.
Speed
Up to 17 in/sec
Electric motion with repeatable positioning and measurable force control.
Built for demanding production environments
The RSX family uses Type III hard-coat anodized aluminum housings and offers an IP67 option for protection against dust and water ingress. Tolomatic positions the platform around precision, ruggedness, lower energy use, simplified maintenance, and consistent performance across industrial temperature ranges.
Read the official announcement: Tolomatic launches the RSX50.
Bring us the application
BEA can help turn force requirements into a practical motion solution
Britton Electronics & Automation can help evaluate the load, stroke, speed, duty cycle, environment, mounting, motor and drive, controls, and safety requirements behind your application. We can also help compare an RSX electric solution with an existing hydraulic approach and coordinate the automation components needed around it.
Contact BEA to discuss a new high-force machine or a hydraulic-to-electric conversion.